

Creality K2 Plus Recommended Filament Parameters Settings
The Creality K2 Plus has been on sale for a year. It is a high-speed 3D printer with a large build volume of 350 × 350 × 350 mm, making it perfect for professionals and small-scale manufacturers. Its ability to print in multiple colours makes it more flexible when working on big, complicated projects.
To get the best print quality, it's very important to set the filament parameters precisely. This includes the nozzle temperature, the bed temperature and how the print cools. Different materials need different configurations to work as well as they should.
This guide gives you recommended filament settings for the K2 Plus, helping you work efficiently with a range of materials and consistently produce high-quality 3D prints.
Creality K2 Plus Recommended Filament Settings
| Parameter | Hyper PLA | ENDER FAST PLA | Hyper ABS | Hyper PLA-CF | HP ASA | Hyper PETG | HP-TPU | CR-TPU | CR-PETG | CR-ABS | CR-PLA | CR-Silk |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Nozzle Temp (℃) | 220 | 220 | 260 | 220 | 260 | 240 | 220 | 220 | 240 | 260 | 220 | 220 |
| Hotbed Temp (℃) | 50 | 50 | 80 | 50 | 90 | 70 | 40 | 40 | 70 | 100 | 50 | 50 |
| Cavity Temp (℃) | 35 | 35 | 50 | 35 | 50 | 35 | 35 | 35 | 35 | 60 | 35 | 35 |
| Pressure Advance | 0.04 | 0.04 | 0.03 | 0.04 | 0.04 | 0.05 | 0.4 | 0.34 | 0.07 | 0.04 | 0.04 | 0.04 |
| Maximum Volume Velocity (mm³/s) | 23 | 23 | 23 | 23 | 14 | 23 | 3 | 2 | 12 | 18 | 18 | 10 |
| Flow Ratio | 0.95 | 0.95 | 0.95 | 0.95 | 0.95 | 0.98 | 1 | 1.02 | 0.95 | 0.95 | 0.95 | 0.95 |
| Cooling Fan (Min/Max) % | 100/100 | 100/100 | 10/60 | 100/100 | 10/40 | 40/80 | 100/100 | 100/100 | 40/80 | 10/60 | 100/100 | 100/100 |
| (Min/Max) Layer Time (s) | 100/4 | 100/6 | 30/12 | 100/8 | 40/10 | 30/8 | 100/8 | 100/8 | 30/8 | 30/12 | 100/4 | 100/4 |
| Cooling Overhang Threshold Value (%) | 50 | 50 | 25 | 50 | 25 | 25 | 95 | 95 | 25 | 25 | 50 | 50 |
| Overhang Fan Speed (%) | 100 | 100 | 80 | 100 | 100 | 100 | 100 | 100 | 100 | 80 | 100 | 100 |
| Parameter | CR-PLA Matte | CR-PLA Fluo | EN PLA+ | Generic PLA | Generic ABS | Generic TPU | Generic PETG | Generic Silk | Generic HIPS | Generic PC | Generic ASA |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Nozzle Temp (℃) | 220 | 220 | 220 | 220 | 260 | 220 | 240 | 220 | 240 | 260 | 260 |
| Hotbed Temp (℃) | 50 | 50 | 50 | 50 | 100 | 40 | 70 | 50 | 100 | 110 | 90 |
| Cavity Temp (℃) | 35 | 35 | 35 | 35 | 50 | 35 | 35 | 35 | 50 | 50 | 50 |
| Pressure Advance | 0.04 | 0.04 | 0.04 | 0.04 | 0.06 | 0.3 | 0.1 | 0.04 | 0.05 | 0.03 | 0.04 |
| Maximum Volume Velocity (mm³/s) | 18 | 18 | 14 | 14 | 16 | 2 | 9 | 8 | 10 | 18 | 14 |
| Flow Ratio | 0.95 | 0.95 | 0.95 | 0.95 | 0.95 | 1 | 0.95 | 0.98 | 0.95 | 0.95 | 0.95 |
| Cooling Fan (Min/Max) % | 100/100 | 100/100 | 100/100 | 100/100 | 10/60 | 100/100 | 40/80 | 100/100 | 30/80 | 10/60 | 10/70 |
| (Min/Max) Layer Time (s) | 100/4 | 100/4 | 100/4 | 100/6 | 30/12 | 100/8 | 30/8 | 80/8 | 30/10 | 30/12 | 40/8 |
| Cooling Overhang Threshold Value (%) | 50 | 50 | 50 | 50 | 25 | 95 | 25 | 50 | 10 | 25 | 25 |
| Overhang Fan Speed (%) | 100 | 100 | 100 | 100 | 80 | 100 | 90 | 100 | 80 | 80 | 80 |
Precautions
1. Drying Process
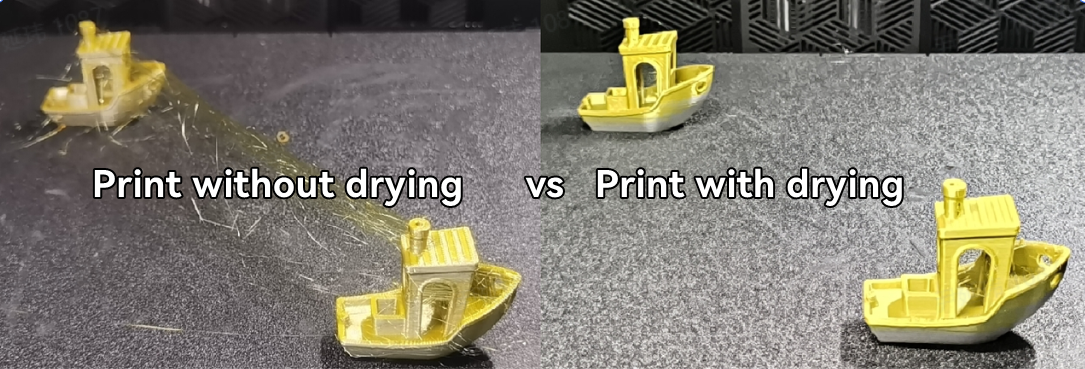
Ensure filaments are dried before and during printing to improve print quality, particularly for materials like PETG, TPU, CR-Silk, CR-PLA Matte, ENDER FAST PLA, and PA (nylon). For detailed drying procedures, refer to Creality's filament drying guide. Proper drying prevents moisture-related defects, enhancing overall print performance.
2. Preventing Warping and Cracking
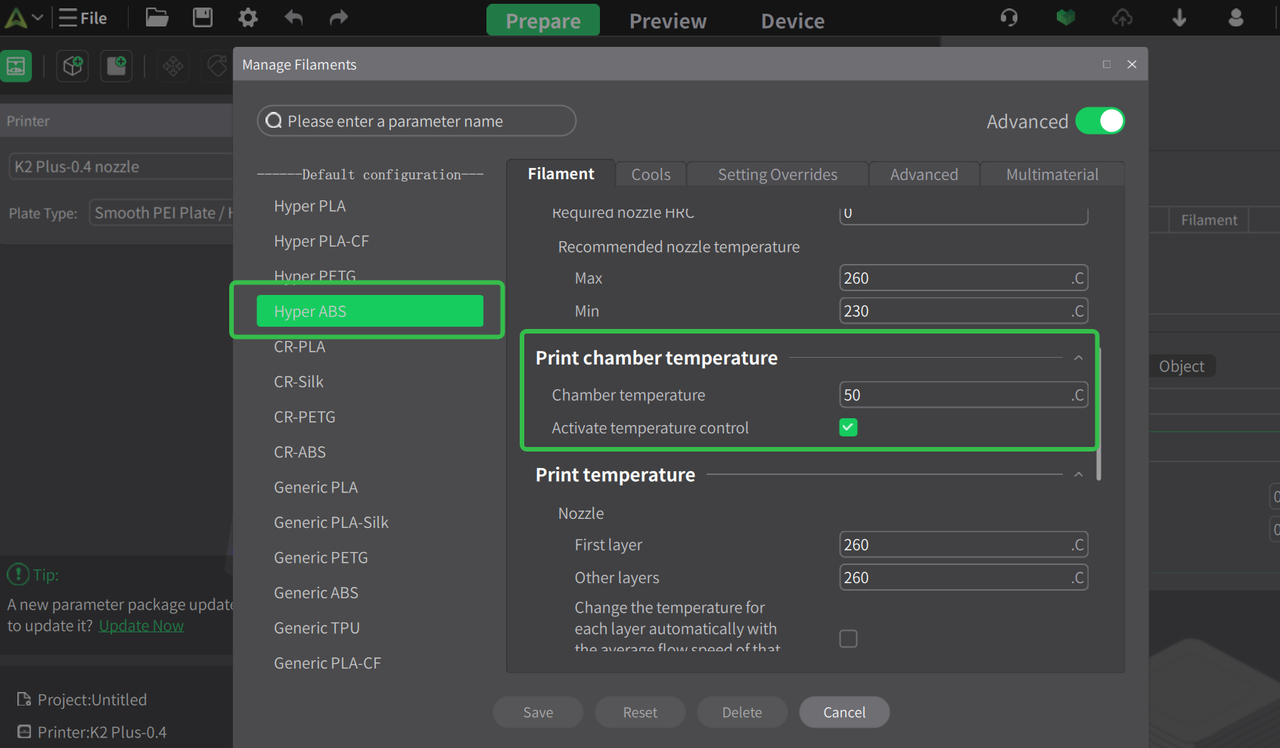
Materials such as ABS, ASA, PC, and PA are prone to warping and cracking due to their inherent properties. To mitigate these issues, use appropriate chamber heating (50-60°C) and close the top cover and front door during printing. Creality Print slicing software has default settings that include chamber heating for these materials.
3. Handling TPU Filament
Avoid using Creality CFS for TPU, as its flexibility can cause feeding issues.
Filaments with a hardness below 85A (e.g., 80A, 75A) are too soft for Creality printers and may lead to extrusion failures or nozzle clogging.
Avoid printing TPU directly through the PTFE tube to minimize resistance and improve print stability.
4. Carbon Fiber Reinforced Materials
For CF materials like PA-CF, PAHT-CF, and PET-CF:
Use a nozzle larger than 0.2mm to prevent clogging. A 0.6mm nozzle is recommended for a balance between precision and reliability.
Set the nozzle temperature between 280-300°C and clean it with a needle before and after use.
Regular maintenance prevents clogs when switching between CF and standard filaments.
5. Default Filament Settings
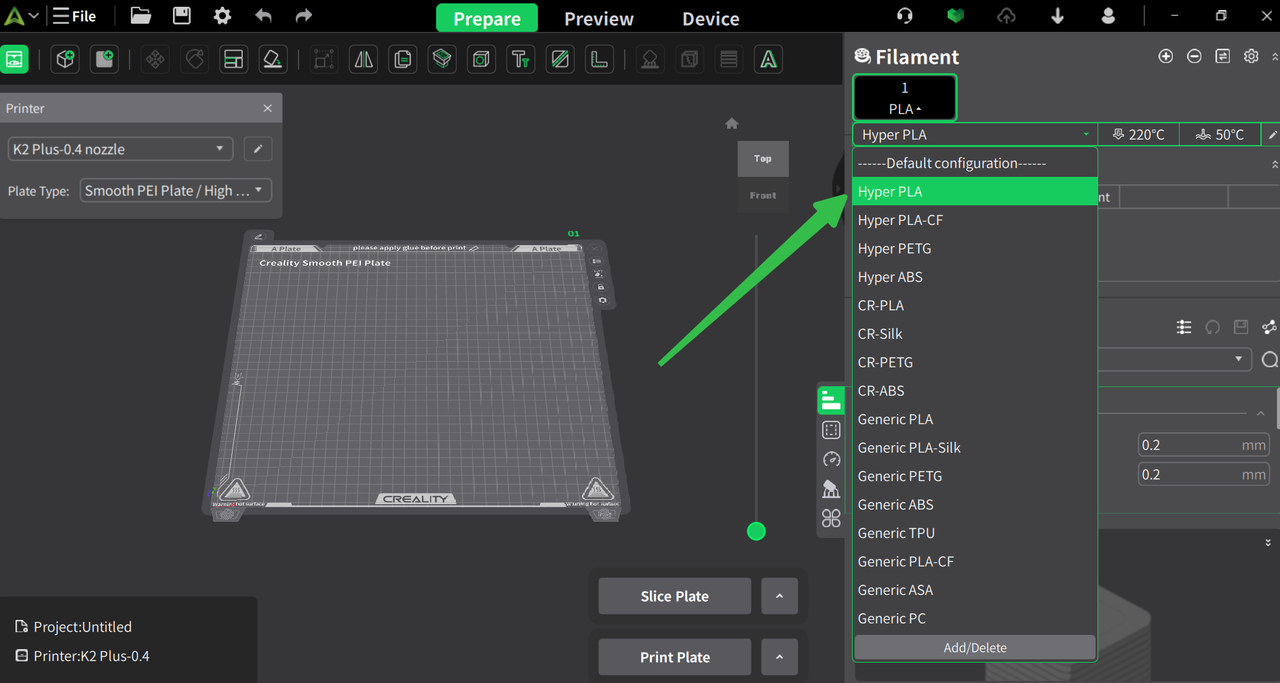
Utilize the built-in parameters in CrealityPrint for optimal performance. Over 40 filament types are pre-configured. If your filament isn't listed, select the closest match.
Parameter Scenarios:
Standard (0.20mm): Balances quality and efficiency, ideal for most prints.
Fine (0.08/0.12/0.16mm): Higher quality, longer print times, not recommended for large multi-color models.
Fast (0.24/0.28mm): Faster prints with lower quality and more noticeable layer lines.
Conclusion
By using the recommended filament settings, users can unlock the full potential of the Creality K2 Plus. Proper parameter tuning not only improves print quality and reliability but also ensures consistent performance across a wide range of materials, making the K2 Plus a dependable solution for demanding 3D printing applications.
Recent News

Creality Ender 3D Printers Compared: Which Printer Is Better for You?

3D Printer Nozzle Blocked? Causes and Safe Fixes

10 Best Back-to-School 3D Prints for Students in 2026
